Accelerating Clean Cooling & Heating

01

Why this matters

Most refrigeration runs on chemicals that warm the planet, or quietly poison it.

HFCs warm the atmosphere up to 14,000× more than CO₂. Their HFO replacements break down into TFA, a forever chemical now detectable in rain, ice, and human blood.

The answer

CO₂, ammonia, hydrocarbons. Proven for over a century. They don't warm the planet, and they don't leave a forever chemical behind.

Natural refrigerants avoid both.

02
Primary metric

A year of avoided emissions, made visible.

GHG emissions Temprite avoided over the lifetime of 2022's equipment placed in the market.

03
In real-world terms

What it adds up to.

256k
homes / year
powered for a year on the same footprint
452k
petrol cars off the road
for one year of driving emissions avoided
5.2B
miles not driven
distance equivalent never burned in a tank
13%
of Phoenix City's
annual city emissions
04

Growth

Cumulative avoided CO₂e emissions over the years.

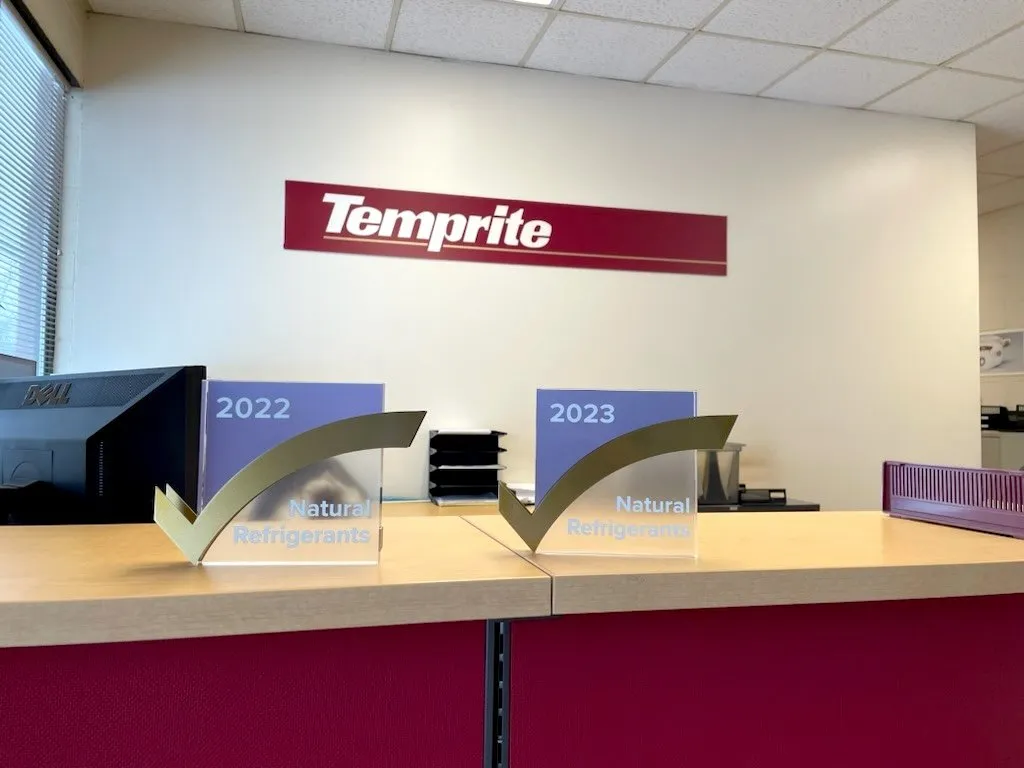
Temprite has been ATMO Approved since 2022, now 2 consecutive years of independently verified impact.

Trajectory bars appear once at least one data year is recorded.

05
Voices from the field

What operators say after a year on natural refrigerants.

Trevor Jacobs
Senior Equipment Design Engineer
Copeland
Performance
How has the system performed over the past year?
Temprite components have been used to support our lab testing practices by managing oil separation. This allows our products to be tested more effectively and consistently.

Mirko Bernabei
Technical Director
SCM FRIGO S.p.A.
Performance
How has the system performed over the past year?
The new Temprite 239A allowed us to build high-capacity refrigeration equipment simplifying the system design and ensuring high performance in oil separation.

Jacob Nielsen
CTO
Fenagy
Performance
How has the system performed over the past year?

Yes, all unit are performance tested and all have successfully reached the guaranteed performance.

Tony McCullough
Global Commodity Manager
Hillphoenix/Dover Food Retail
Quality & Reliability
How has the build quality and reliability held up?

We have not experienced any quality or reliability related issues with Temprite's products.

Trevor Jacobs
Senior Equipment Design Engineer
Copeland
Quality & Reliability
How has the build quality and reliability held up?

Temprite components have been reliable in our applications in a lab environment. This allows our group to maximize the available testing schedules.

Mirko Bernabei
Technical Director
SCM FRIGO S.p.A.
Quality & Reliability
How has the build quality and reliability held up?

The oil separator shows high reliability and easy maintenance.

Tony McCullough
Global Commodity Manager
Hillphoenix/Dover Food Retail
Service
How was the level of service and technical support?

Communication & on time delivery are always on point.

Trevor Jacobs
Senior Equipment Design Engineer
Copeland
Service
How was the level of service and technical support?

Temprite has always been supportive and responsive to our customer needs. We have been given help to select appropriate hardware and have received orders in a timely manner.

Mirko Bernabei
Technical Director
SCM FRIGO S.p.A.
Service
How was the level of service and technical support?

Temprite helps us with the selection of the components and ensures the fastest delivery.

Tony McCullough
Global Commodity Manager
Hillphoenix/Dover Food Retail
Safety
How has safety been operating natural refrigerants?

Yes, Temprite has extremely robust internal testing procedures.

Trevor Jacobs
Senior Equipment Design Engineer
Copeland
Safety
How has safety been operating natural refrigerants?

Temprite components have always functioned safely in our applications. Temprite provides literature describing safe installation of their products.

Mirko Bernabei
Technical Director
SCM FRIGO S.p.A.
Safety
How has safety been operating natural refrigerants?

Yes. They gave us full support on the selection and design of the installation.

Tony McCullough
Global Commodity Manager
Hillphoenix/Dover Food Retail
Satisfaction
Would you work with this company again?

Absolutely, will definitely consider Temprite for future projects.

Trevor Jacobs
Senior Equipment Design Engineer
Copeland
Satisfaction
Would you work with this company again?

We plan to use Temprite in the future to continue supporting our lab testing equipment. Temprite products have proven to be effective and reliable in our applications.

Mirko Bernabei
Technical Director
SCM FRIGO S.p.A.
Satisfaction
Would you work with this company again?

Yes, they are always very committed also in supporting us with new and advanced products.

06
The company

Temprite: company profile.

Temprite continues its long-standing tradition of innovation with energy-efficient coalescent and conventional oil separators, designed for use with all types of refrigerants. Among its flagship products is the 130 Series of coalescent oil separators, specifically engineered for transcritical CO₂ systems. These products are built to enhance thermal efficiency by reducing oil and particulate contamination in the evaporator, leading to shorter compressor run times, lower energy consumption, reduced carbon emissions, and a higher return on investment.

Work with Temprite

Tell us about your project. We'll route the conversation to the right team.
Get in touch

Become ATMO Approved

Does your company use natural refrigerants?

The ATMO Approved label is independently verified. Not self-declared, not marketing. If your equipment runs on CO₂, ammonia, hydrocarbons, or water, you may qualify.